Buyer Guides
Thermal Vias with Thick Copper: Design Optimization
Jun
A hot board lies.
I’ve watched a PCB look “safe” on the bench, pass a quick load test, sit proudly under an IR camera for five minutes, and then — once it’s inside a sealed enclosure with no real airflow — crawl into ugly temperature numbers that nobody wanted to explain.
It happens. A lot.
And here’s the ugly truth: Thermal Vias don’t fix bad thermal thinking. They only expose it faster.
People love thick copper because it feels decisive. More copper. More current. More heat spreading. Done, right?
Not really.
In Thick Copper PCB Design, heat doesn’t care how confident the layout looks. It cares about path resistance, copper continuity, via barrel geometry, solder voids, plane size, enclosure contact, and whether that “thermal pad” is connected to something useful or just a decorative island of copper.
I frankly believe many power PCB mistakes start from one lazy sentence: “Just add more vias.”
That sentence burns money.
Why Thermal Vias Become More Serious When Copper Gets Thick
But before we blame the via, let’s blame the assumption.
Thermal Vias are plated or filled holes that move heat from a hot surface layer into inner copper, bottom copper, chassis contact, heat sink zones, or large spreading planes. In normal FR-4 boards, they’re already useful. In heavy copper boards, they become more political — because every extra hole fights with routing space, copper balance, soldering, drill limits, and plating control.
Small holes. Big consequences.
A via barrel isn’t a solid copper rod unless you paid for something closer to that. Standard plated through holes mostly conduct through their wall plating. The center is usually air, resin fill, or whatever via process was selected. So when someone calculates heat transfer as if every via is a solid copper plug, I get nervous.
Very nervous.
A multilayer motor-control PCB with power circuits is a good example. Motor drivers don’t politely generate heat in one neat square. You get MOSFET loss, copper loss, switching noise, connector heating, current loop constraints, and sometimes a layout that looks fine until the product actually starts pushing load.
Thermal Via Design lives inside that mess. It’s not a separate decoration layer.
The Thick Copper Trap: More Copper Can Make the Layout Worse
Here’s the part buyers don’t always hear from factories: thick copper helps, but it also removes options.
Go from 1 oz to 2 oz, then 3 oz, and suddenly fine spacing isn’t so friendly. Etching compensation gets less forgiving. Solder mask dams get angry. Annular rings need more respect. CAM engineers start asking questions nobody asked during schematic review.
And yes, this is where cost begins to creep.
A 3 oz or 4 oz outer layer may spread heat better than 1 oz, but it can also force wider traces and spacing. If the PCB has high-current switching areas mixed with fine-pitch control signals, the designer needs to zone the board early. Don’t leave that argument for the quote stage. That’s how projects lose a week.
Or two.
A custom control PCB with connector-rich layout can look simple at first glance. But connectors block airflow, pull current through narrow areas, and often force copper pours into awkward shapes. Add Thermal Vias without thinking about return paths and real copper area, and you’ve just drilled holes into a weak plan.
Not thermal engineering. Just hole punching.
Thermal Via Array Design: Stop Counting Holes Like Beads
The first question is usually wrong.
“How many thermal vias should I use?”
Fine. I understand why people ask. But I’d rather hear: “Where does the heat go after it enters the via?”
Because if the answer is “into a tiny bottom copper patch under solder mask with no chassis contact,” then congratulations — you moved the heat 1.6 mm downward and still trapped it in the PCB.
That’s not enough.
A Thermal Via Array Design needs a destination. Inner plane. Bottom plane. Exposed copper. Aluminum carrier. Thermal pad. Metal enclosure. Airflow path. Something. Heat needs a way out, not just a short trip downstairs.
| Design Variable | Good Practice | Common Mistake | Why It Matters |
|---|---|---|---|
| Via diameter | Often 0.20–0.40 mm finished hole for dense thermal pads | Oversized vias that steal solder or routing space | Diameter affects copper cross-section, filling choice, and solder behavior |
| Via pitch | Tight enough to spread heat, not so tight that copper plane is damaged | Blindly using a square grid everywhere | Pitch affects heat spreading and manufacturability |
| Copper plating | Confirm barrel plating and finished hole expectations | Assuming via walls equal solid copper | Most vias are mostly air unless filled or capped |
| Via filling | Use copper filling or conductive filling when the design justifies cost | Choosing filling without assembly reason | Filling changes cost, planarity, and heat transfer |
| Plane connection | Connect to real copper planes or bottom-side heat spreaders | Vias ending in isolated copper islands | Heat needs a destination |
| Solder control | Tent, plug, cap, or fill depending on pad type | Open vias under exposed pads causing solder drain | Assembly yield can fail before thermal design is tested |
I’ve seen a dense via grid perform worse than a cleaner, wider copper pour with fewer but better-connected vias. Sounds annoying, doesn’t it?
But it’s true.
Extra vias can start eating copper. They can weaken a pad field. They can create solder wicking. They can complicate stencil decisions. They can make inspection less pleasant. The thermal gain isn’t always linear. Past a certain point, you’re paying for process risk more than temperature drop.
Copper Filled Thermal Vias: Good Tool, Bad Religion
Copper Filled Thermal Vias get over-sold.
There, I said it.
They can absolutely help when the design needs stronger vertical heat transfer, flat pads, via-in-pad assembly, or reduced solder wicking. For exposed-pad packages, compact power ICs, RF modules, LED thermal pads, and small high-current layouts, copper filling can be worth the money.
But don’t worship it.
A copper-filled via isn’t a magic heat elevator. If it lands in a poor plane, the benefit is limited. If the board has no real heat exit path, copper fill just makes the local structure nicer — not necessarily the product cooler.
Ask the rough questions first. Is the via inside the solderable exposed pad? Will open vias drain solder? Is voiding acceptable? Does the component supplier specify via-in-pad treatment? Will ENIG and capping be needed for planarity? Is the product space-limited enough to justify the process?
For high-frequency designs, this gets even more touchy. Thermal copper can disturb impedance if someone dumps metal around a sensitive route without thinking. A design like an OEM high-frequency 6-layer PCB with ENIG pads needs the thermal plan checked beside signal integrity, return current, dielectric choice, and via stubs.
Heat and RF don’t live in separate rooms.
How to Optimize Thermal Vias with Thick Copper
Start ugly. Start with watts.
Not with pretty via grids. Not with a screenshot. List the heat sources: MOSFETs, shunts, inductors, charging ICs, regulators, LEDs, power resistors, connectors, gate drivers, and any part that gets suspiciously warm during real load.
Then estimate loss. Even rough numbers beat guessing.
A 0.8 W regulator, a 2.5 W MOSFET, and a 6 W LED driver shouldn’t receive the same via strategy. Yet I still see layouts where everything gets the same grid because the footprint library made it convenient.
Convenient is dangerous.
After that, define the exit path. Bottom copper? Internal 2 oz plane? Metal case? Aluminum heat spreader? Thermal pad to enclosure? Forced air? Natural convection? If there’s no answer, Thermal Vias are just moving heat into a dead-end structure.
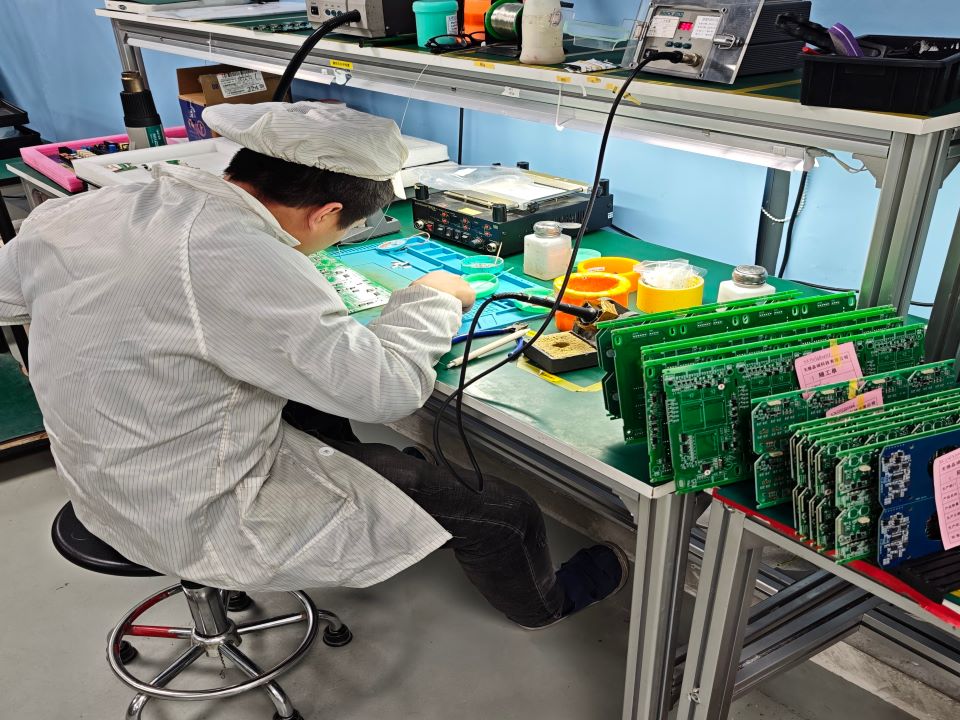
A custom double-sided prototype PCB panel may be fine for quick validation, especially when the power level is modest. But once the design moves toward production, prototype data should drive decisions on copper weight, via fill, surface finish, stack-up, solder mask openings, and whether the thermal area needs mechanical contact.
Don’t guess twice.
Heavy Copper PCB Thermal Management Is Also a Reliability Problem
However, temperature is only the headline.
The quiet damage is cycling. A PCB that reaches 90°C once may survive. A PCB that jumps from 30°C to 95°C every shift, every day, under vibration or load pulsing — that board starts collecting fatigue in solder joints, copper barrels, resin interfaces, and connector areas.
Heavy copper can help spread heat. It can also increase mechanical stress if copper distribution is unbalanced. Large copper areas pull differently than resin-rich areas. Dense via farms can add plating stress. Thick copper near flexible sections can become a long-term crack invitation.
This is why I’d never copy a rigid-board via strategy into flex or rigid-flex without slowing down.
A polyimide rigid-flex PCB with FPC cable has a different failure personality. Bend radius, adhesive system, copper grain direction, stiffener placement, and thermal exposure all matter. Thermal vias may help in the rigid zone, but the flex section doesn’t forgive lazy copper choices.
It remembers.
Practical Design Rules I’d Actually Start With
I don’t trust universal via rules.
Too many articles pretend there’s one perfect number. There isn’t. A motor driver, LED PCB, RF amplifier, battery BMS, and USB power board all behave differently. Even two boards with the same schematic can run differently if enclosure contact changes.
Still, for first-pass review, I’d use this as a practical starting frame:
| Item | Practical Starting Point | When to Adjust |
|---|---|---|
| Outer copper | 2 oz for moderate power, 3 oz+ for higher current zones | Increase if lateral spreading or current density demands it |
| Thermal via finished hole | 0.20–0.40 mm | Use larger holes if fabrication and spacing allow |
| Via pitch | 0.50–1.20 mm depending on pad size and copper area | Tighten under hot spots, loosen where routing or soldering suffers |
| Via type | Plated through-hole thermal vias | Consider blind, buried, filled, or capped vias if space or assembly requires it |
| Filling | Non-conductive, conductive, or copper fill depending on need | Copper fill for stronger thermal transfer and pad planarity, but check cost |
| Surface finish | ENIG often used for flat pads and assembly consistency | HASL may be less ideal for fine exposed-pad thermal areas |
| Validation | Thermal simulation plus prototype measurement | Use thermocouples, IR camera, and load testing inside real enclosure |
Notice the missing command: “add maximum vias.”
Good.
PCB Heat Dissipation Vias should be sized around component loss, layer count, board thickness, copper weight, finished hole size, solder process, and where the heat is meant to leave. If that sounds less exciting than a rule of thumb, that’s because real PCB work usually is less exciting.
But it ships better.
What a Serious PCB Factory Will Push Back On
And this is where supplier quality shows.
A weak factory says yes to everything. A useful factory asks why.
For thick copper boards, the review shouldn’t stop at Gerber import. It should check trace/space under heavy copper, copper balance, annular ring, drill-to-copper clearance, via filling method, plating tolerance, solder mask dams, exposed-pad treatment, final thickness, surface finish, impedance zones, and whether the assembly process can survive the thermal pad design.
That’s the boring work. It saves projects.
Even a product that looks more “interface” than “power” can have local heat zones. An OEM FR4 USB interface PCB with blue solder mask may include power switching, ESD protection, charging paths, regulators, or connector current. These areas don’t care that the board isn’t marketed as a power PCB.
They still heat up.
So when your PCB supplier asks about current, load time, enclosure, copper weight, and via treatment, don’t treat it as friction. Treat it as risk control. The cheapest answer usually arrives fast. The better answer may ask for one more file.
Annoying? Yes.
Useful? Also yes.
FAQ
What are Thermal Vias in thick copper PCB design?
Thermal Vias in thick copper PCB design are plated or filled holes that transfer heat from hot component areas into inner copper layers, bottom copper, or external heat-spreading structures while thick copper improves lateral heat distribution across the PCB surface and planes. They work best when the full heat path is planned.
But the via itself is not the whole solution. If it connects to a small isolated copper patch, the improvement may be disappointing. If it connects to a strong plane, metal housing, or bottom-side heat spreader, the result can be much better.
How do you optimize Thermal Vias with thick copper?
To optimize Thermal Vias with thick copper, define the heat source, choose the heat exit path, size the via array, connect it to real copper planes, control solder behavior, and confirm manufacturability before production. The design should balance thermal gain, routing space, plating limits, and assembly yield.
From my experience, the best starting point isn’t via count. It’s heat flow. Once you know where the watts are going, you can choose copper weight, via pitch, filling, surface finish, and stack-up with less guessing.
Are copper filled thermal vias better than standard plated vias?
Copper filled thermal vias are better when vertical heat transfer, exposed-pad planarity, solder control, and compact package reliability matter enough to justify higher process cost. Standard plated thermal vias may be enough when the via array is outside the solder pad and connects to large copper areas.
The trap is assuming copper fill always wins. Sometimes it does. Sometimes a standard plated via array with better plane connection, wider copper spreading, and cleaner assembly behavior gives the more practical result.
Does thicker copper always improve PCB heat dissipation?
Thicker copper often improves lateral heat spreading, but it does not always improve total PCB heat dissipation if the vertical path, copper plane connection, airflow, enclosure, or external heat sink is weak. Heavy copper helps most when it connects heat sources to a larger usable thermal mass.
A thick copper island can still be a hot island. If the copper has nowhere to send heat, it only delays the problem. It doesn’t solve it.
What is the best thermal via array design?
The best thermal via array design uses enough plated or filled vias to move heat vertically while preserving solder quality, copper plane strength, routing space, and manufacturability. Typical decisions include via diameter, pitch, filling type, pad placement, plane connection, and whether vias sit inside or outside solderable pads.
I don’t believe in one perfect grid. MOSFETs, LEDs, regulators, shunts, and connector zones all need different treatment. The best array is the one that matches the component loss and the real heat exit route.
When should I ask my PCB supplier to review thermal vias?
You should ask your PCB supplier to review thermal vias before final routing, not after Gerber export, because copper weight, via filling, solder mask openings, stack-up, drill limits, and assembly process can change the layout. Early review prevents expensive redesign and avoids false thermal assumptions.
If the PCB has high current, enclosed operation, hot packages, thick copper, or dense power areas, send the stack-up and thermal notes early. Waiting until mass production is how small layout mistakes become expensive arguments.
Conclusion
If your PCB has hot MOSFETs, LED drivers, battery circuits, motor-control sections, regulators, or dense power areas, don’t treat Thermal Vias like a last-minute patch. Send the stack-up, copper weight target, Gerber files, BOM, and heat-source notes before production. We can help check whether your thick copper PCB design only looks strong — or actually has a heat path that can survive real operating conditions.
