Buyer Guides
PCB Stackup Design for High-Frequency Impedance Control
Jun
I’ve seen a 50Ω line fail before the factory even touched the laminate.
No drama. No mystery. Just a stackup that looked “close enough” on a drawing, while the actual dielectric height, finished copper, solder mask, and etch compensation were all floating around like nobody owned them.
That’s where PCB stackup design gets ugly.
People love saying “controlled impedance” as if the phrase itself controls anything. It doesn’t. It’s only useful when the designer, CAM engineer, material buyer, press room, and test team are all working from the same physical assumptions. Otherwise, it’s just two words on a fabrication note.
And yes, I frankly believe this is where many high-frequency PCB projects lose money.
Not at SMT.
Not at final assembly.
At stackup.
The stackup is not a layer list
L1 signal. L2 ground. L3 power. L4 signal.
Nice. Useless.
Well, not totally useless, but it’s nowhere near enough for high frequency PCB stackup work. A real stackup tells us copper thickness after plating, dielectric thickness after pressing, Dk at the working frequency, Df, glass style risk, solder mask assumption, reference plane condition, and which traces are being modeled as microstrip, embedded microstrip, stripline, or differential stripline.
Here’s the ugly truth: if a drawing only says “controlled impedance ±10%” but gives no material class, no finished copper, no target structure, and no stackup table, then the factory has to guess.
Some factories guess carefully.
Some guess cheaply.
Guess which one wins the first quotation round?
Impedance doesn’t care about your intention
A trace doesn’t become 50Ω because the engineer typed 50Ω into a note.
It becomes 50Ω because the field sees a specific geometry: trace width, copper height, dielectric distance, dielectric constant, reference plane, solder mask, and nearby copper. Move one part of that structure, even slightly, and the number moves.
Tiny shift. Big noise.
On a slow relay control PCB, maybe nobody notices. On RF, radar, GNSS, Wi-Fi, mmWave sensing, 5G modules, fast SerDes, or high-speed medical electronics, that same “small” shift can show up as return loss, insertion loss, eye diagram collapse, phase drift, EMI trouble, or one of those painful lab comments: “prototype works sometimes.”
Sometimes is expensive.
For an automotive electronics control PCB prototype, stackup decisions may need to balance impedance, vibration, copper current, thermal stress, and long-term reliability. That’s not the same job as building a simple two-layer FR-4 sample.
Microstrip is exposed. Stripline is buried.
Simple words.
But in the shop, they mean very different problems. Microstrip sits on the outer layer, so solder mask, surface finish, plating thickness, and etch profile get involved. Stripline sits inside the board, so lamination thickness, resin flow, prepreg selection, and inner-layer copper control matter more.
Which one is better?
Bad question.
The better question is: which structure can hit the electrical target and still be built repeatedly without asking the factory to perform magic every production lot?
Because I’ve seen beautiful impedance simulations that were basically fantasy once the stackup moved into real prepreg, real copper, real press cycles, and real panel compensation.
Factory reality bites.
The real variables behind PCB impedance control
| Stackup factor | Why it matters for impedance | Common risk in real production | What to confirm before fabrication |
|---|---|---|---|
| Dielectric thickness | Sets distance from trace to reference plane | Prepreg resin flow changes final thickness | Target finished dielectric, not only nominal prepreg |
| Dk value | Changes signal velocity and impedance | Dk varies by material, frequency, resin, and glass style | Use material data at working frequency |
| Copper thickness | Wider or taller copper changes impedance | Plating increases outer-layer copper | Finished copper thickness after plating |
| Trace width and spacing | Directly controls single-ended and differential impedance | Etching creates trapezoid trace shape | Factory compensation rules |
| Reference plane | Provides return path and field control | Plane splits create discontinuity | Continuous GND under high-speed routes |
| Solder mask | Affects surface microstrip impedance | Thickness is not perfectly uniform | Whether solder mask is included in impedance model |
| Via transition | Adds inductance, capacitance, and stub effects | Long stubs hurt RF and fast edges | Back drilling, blind vias, or shorter transitions |
| Surface finish | Slight effect on loss and solderability | Roughness and finish choice affect high frequency behavior | ENIG, OSP, immersion silver, or other finish |
This table is not academic decoration.
It’s the checklist that separates “we quoted a PCB” from “we understood the signal path.” If the RFQ doesn’t say whether copper is base copper or finished copper, someone will assume. If the stackup doesn’t say whether solder mask is included in the microstrip model, someone will assume again.
Assumptions stack up.
Then impedance drifts.
FR-4 is not the villain. Lazy FR-4 selection is.
I don’t hate FR-4.
Actually, for many high-speed digital boards, controlled FR-4 can be completely fine. Short routing, reasonable rise time, modest loss budget, stable supplier process, clean reference planes—that can work.
But RF is less forgiving.
When people use one generic Dk number like it’s carved into stone, I get nervous. Dk moves with frequency, resin content, glass weave, test method, and laminate family. Df matters too, especially when insertion loss starts becoming a real performance limit instead of a datasheet footnote.
So no, “FR-4 Tg170” does not automatically mean “good for high frequency.”
Different question.
For LED or thermal boards, the stackup conversation moves in another direction. A 15W circular aluminum LED PCB is usually not about RF impedance, but it proves the same manufacturing law: material is not just a purchasing line item. Material decides performance.
The quote that looks cheaper may not be cheaper
Two factories quote the same 6-layer PCB.
One uses a specific laminate, confirms finished copper, includes controlled impedance testing, and adjusts trace geometry after CAM review. The other quotes “FR-4 equivalent,” assumes nominal prepreg, skips the coupon detail, and gives a lower unit price.
On paper, both are “6-layer PCB.”
In reality? Not the same product.
I’ve seen buyers compare these prices like they’re comparing screws. They’re not. A controlled impedance PCB design is part material engineering, part signal integrity, part process control. If you strip out the technical assumptions, of course the price looks cleaner.
Clean number. Dirty risk.
For a multilayer motor control PCB with power circuit, this gets even more uncomfortable because power copper, switching noise, heat, and signal routing can all sit inside the same board. That’s where stackup shortcuts become field problems.
Connector areas ruin more signals than people admit
Long straight traces get all the attention.
But the connector launch often does the damage.
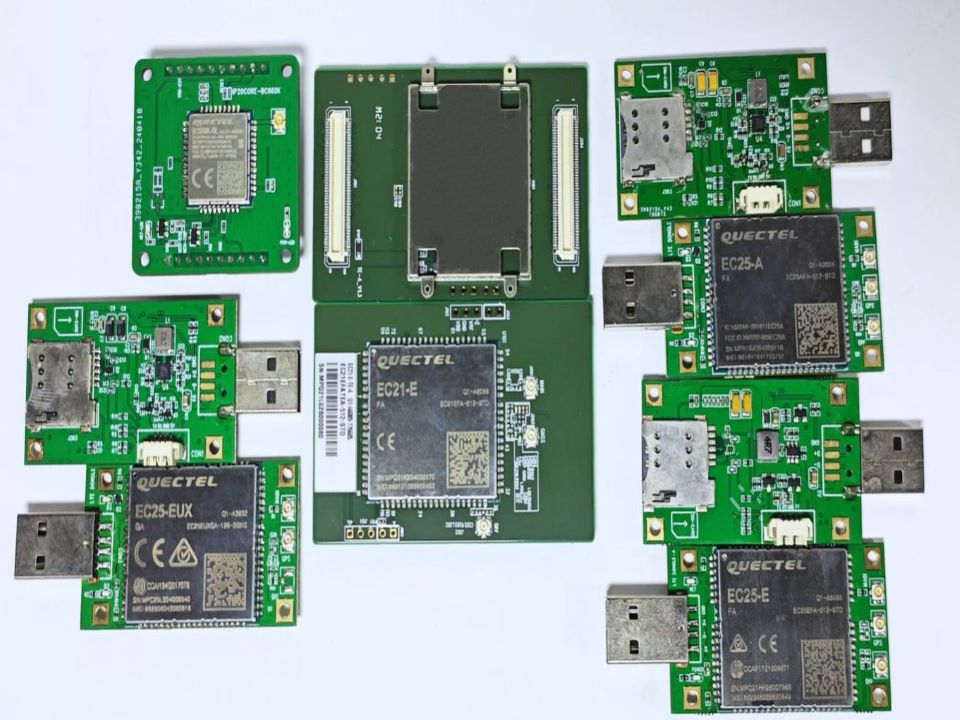
A route can be beautifully controlled for 80 mm, then get wrecked in the last 5 mm near a connector because the ground reference changes, the pair necks down, the anti-pad is too aggressive, the via stub is too long, or the nearby copper pour changes the field.
That’s the kind of thing a basic impedance calculator won’t save.
For a custom control PCB with connector-rich layout, I’d rather review the launch geometry early than argue later about why the TDR coupon passed but the product still behaves badly.
Yes, coupons help.
No, coupons don’t forgive bad routing.
Rigid-flex makes the stackup conversation even less forgiving
Rigid-flex is where casual stackup thinking really starts to hurt.
Polyimide isn’t FR-4. Bend areas aren’t normal rigid areas. Adhesive, coverlay, copper type, bend radius, stiffener location, and rigid-to-flex transitions all change what the signal “sees.” If controlled impedance crosses that transition, you’d better know what geometry exists on both sides.
Don’t wing it.
A polyimide rigid-flex PCB with FPC cable needs early stackup review because the mechanical and electrical design are tied together. Move the bend zone, and you may move the impedance condition. Change the copper type, and you may change reliability.
This is why I dislike late-stage “just quote it” RFQs for rigid-flex.
Too many hidden traps.
What I want to see before I trust the stackup
Not a pretty PDF.
A useful stackup.
Give me the material family, Dk, Df, finished dielectric thickness, copper thickness before and after plating, surface finish, impedance targets, tolerance, line width, spacing, reference plane, solder mask assumption, and test coupon requirement.
Then I can actually review something.
A good RFQ for high-frequency impedance control should include:
- Layer count and finished PCB thickness
- Target impedance values, such as 50Ω, 75Ω, 90Ω, or 100Ω
- Tolerance, usually ±5%, ±8%, or ±10%
- Material requirement or electrical requirement
- Finished copper thickness
- Controlled impedance layer and structure
- Surface finish
- Test coupon and test report requirement
- Prototype quantity and production quantity
- Application type, such as RF module, sensor, telecom, automotive, medical, or industrial control
Too much?
No.
This is cheaper than rebuilding the board.
A 50Ω example that happens all the time
A customer sends a 4-layer PCB and asks for 50Ω on L1.
The trace is already routed. Mechanical outline fixed. Connector fixed. PCB thickness fixed. The customer wants quick samples because the project schedule is already late—of course it is—and the fab note says “controlled impedance.”
Then CAM calculates it.
Problem.
With the current dielectric distance between L1 and L2, the trace needs to be wider than the layout allows. Or the dielectric must be thinner. Or the material Dk must change. Or the stackup must be rebuilt.
Now everyone is annoyed.
But the stackup didn’t fail suddenly. It was never confirmed in the first place.
A 100Ω differential pair is not just two 50Ω traces
This mistake refuses to die.
Differential impedance depends on trace width, spacing, dielectric height, copper thickness, reference plane, solder mask, and coupling strength. If the pair is loosely coupled, each line behaves closer to its own single-ended structure. If the pair is tightly coupled, the process window becomes more sensitive.
And then the breakout region happens.
USB, LVDS, MIPI, Ethernet, PCIe, sensor links—whatever the interface is, the straight section may be fine while the escape area near the connector is a mess. Neck-downs, asymmetry, missing ground stitching, layer changes without return vias, long stubs. The usual suspects.
From my experience, the layout doesn’t usually fail in the part everyone checked.
It fails in the part someone assumed was “too short to matter.”
Don’t ask the calculator to do the engineer’s job
Impedance calculators are useful.
They’re also dangerous when people treat them like authority instead of a model. The calculator only knows what you feed it. Wrong Dk? Wrong answer. Wrong copper thickness? Wrong answer. Solder mask ignored? Maybe wrong again. Real trace shape after etching? Not perfectly rectangular, sorry.
This is why factory feedback matters.
For a custom double-sided prototype PCB panel, the stackup may be simple enough to move quickly. But for RF PCB stackup or multilayer PCB stackup work, the model must be checked against the actual process capability.
Otherwise, the calculator gives confidence.
False confidence.
What I check before production release
| Review item | Acceptable practice | Red flag |
|---|---|---|
| Stackup file | Shows materials, copper, dielectric, impedance model | Only shows layer names |
| Impedance target | Defines 50Ω, 75Ω, 90Ω, 100Ω, etc. with tolerance | Says “control impedance” only |
| Material | Specifies laminate or electrical class | Says “FR-4 equivalent” for RF work |
| Reference plane | Continuous GND under signal | Plane split under RF/high-speed line |
| Via design | Short stub, back drill, blind via, or controlled transition | Long unused via barrel |
| Coupon | Matches key structures | Generic coupon unrelated to real routing |
| Supplier feedback | CAM engineer reviews stackup before production | Factory only confirms price and lead time |
I know this looks basic.
But basic is where projects bleed.
A missing reference plane split, one sloppy “equivalent material” note, or one ignored via stub can cost more than the entire prototype batch. And when the product is already in customer testing, nobody wants to hear that the fix requires rerouting.
How to design PCB stackup for impedance control
Start with the signal target, not the layer count.
Choose the impedance first. Confirm the signal type. Decide microstrip or stripline. Lock the reference plane. Pick the material. Confirm Dk and Df at the working frequency. Set finished copper. Calculate trace width and spacing. Then ask the PCB manufacturer whether the structure is actually buildable.
That last step matters.
A good supplier won’t just say yes. A good supplier will push back when the dielectric is unrealistic, when the trace width is too tight, when copper weight fights impedance, or when your “equivalent material” note is asking for trouble.
That pushback may feel annoying.
It’s valuable.
FAQ
What is PCB stackup design for high-frequency impedance control?
PCB stackup design for high-frequency impedance control is the planning of PCB layers, dielectric thickness, copper weight, material Dk/Df, reference planes, and impedance structures so RF or high-speed signals can move with predictable electrical behavior. It turns an impedance target into a manufacturable board structure.
The important point is this: the stackup is not only a design file. It’s a manufacturing agreement. If the engineer and factory don’t agree on finished copper, dielectric spacing, solder mask effect, and impedance test method, the final PCB may not match the simulation.
What is the difference between microstrip and stripline impedance?
Microstrip impedance uses a signal trace on an outer layer referenced to an internal plane, while stripline impedance uses a signal trace buried between two reference planes. Microstrip is more exposed to solder mask and air effects; stripline depends more on lamination thickness and dielectric control.
In simple words, microstrip is easier to access but more exposed to process variation. Stripline is more shielded, but the press process becomes more important. Neither is automatically better. The right choice depends on frequency, loss target, routing space, and manufacturing tolerance.
Why does dielectric constant matter in PCB impedance control?
Dielectric constant, usually called Dk, matters because it affects how electromagnetic energy travels through PCB material and directly changes impedance, delay, wavelength, and signal behavior. A higher Dk usually lowers impedance for the same trace geometry, while Dk variation can shift RF performance.
The trap is using one generic Dk number for every frequency. That’s lazy. For high-frequency PCB stackup work, material data should match the actual operating frequency as closely as possible, especially when insertion loss or phase stability matters.
Is FR-4 good enough for high-frequency PCB stackup design?
FR-4 can be good enough for some high-speed or moderate-frequency PCBs, but it is not automatically suitable for RF, microwave, mmWave, radar, or low-loss designs. The decision depends on frequency, trace length, rise time, loss budget, impedance tolerance, and product reliability requirements.
So yes, FR-4 can work. But don’t hide behind the name. The material family, resin system, glass style, Dk, Df, and supplier process all matter. For tighter RF designs, low-loss laminates are often the safer choice.
When should impedance be checked with the PCB manufacturer?
Impedance should be checked with the PCB manufacturer before layout is locked and before Gerber files are finalized. Early review helps confirm trace width, spacing, dielectric thickness, finished copper, material availability, and realistic impedance tolerance before the design becomes expensive to change.
Waiting until after routing is risky. If the required trace width doesn’t fit, or the dielectric stack can’t be built with normal material, someone has to reroute, change the stackup, or accept electrical risk. None of those options feel good late in the schedule.
What information should be included in a controlled impedance PCB RFQ?
A controlled impedance PCB RFQ should include layer count, finished thickness, target impedance, tolerance, material requirement, copper thickness, impedance layer, surface finish, test coupon needs, application type, and prototype or production quantity. These details let the factory quote the real technical build.
Without that information, the supplier is forced to assume. And assumptions make price comparisons almost meaningless. One quotation may include impedance testing and stable laminate control; another may be based on a cheaper generic stackup. Same “PCB” label. Very different risk.
Conclusion
If your project involves RF, high-speed digital, automotive sensing, industrial control, connector-heavy layouts, or rigid-flex transitions, don’t leave impedance control as a late-stage factory guess.
Send us your Gerber files, target stackup, impedance values, material notes, and quantity plan. We can review the PCB stackup design, check manufacturability, and help adjust the high-frequency PCB stackup before small layout choices turn into expensive test failures.
